image

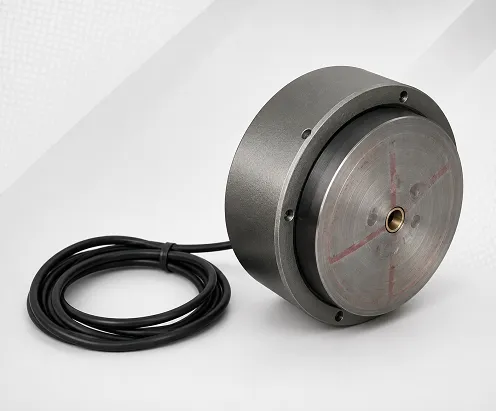
Circular Electromagnetic Chuck for Cylindrical Grinding Machine

Magnetic Chucks for Grinding & Milling Operations

Circular Electromagnetic Chuck for Cylindrical Grinding Machine

Application

This circular electromagnetic chuck is designed for cylindrical grinding machines and generates strong magnetic force to hold the workpiece rigidly.

It operates on continuous D.C. power. There is no internal wear or deformation caused by moving internal parts, providing a longer life than a conventional permanent magnetic chuck.

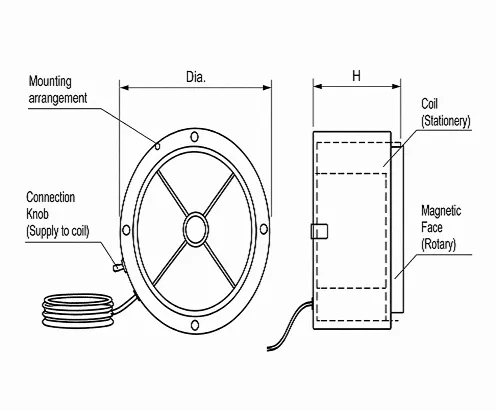
Stationary-Coil Arrangement

The coil remains stationary while the middle magnetic face is connected to the machine spindle and rotates during cylindrical grinding. Accuracy is maintained as per IS 8710-1978.

Construction of Electromagnetic Chuck

  • Fabricated overall body made from high-permeability steel.
  • Pole separation using brass strips.
  • Enamelled copper-wire conductor.
  • Class-H insulation with an FRP winding former.
  • Epoxy-potting bonding and continuous D.C. operation.
  • Operation through an operating pendant.
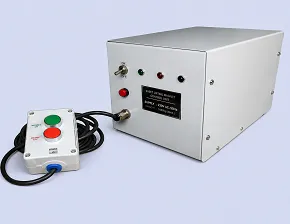
Characteristics of Control Panel

  • Input power supply: 230 V A.C.
  • Output operating voltage: 110 V D.C.
  • A.C. and D.C. supplies protected by fuses and MCB.
  • Indicators for main supply, Magnet ON and demagnetizing cycle.

Inspection & Accessories

Inspection tests:
1) Resistance-to-earth terminal test
2) Demagnetizing test
3) High-voltage test
4) Leak-proof test
5) Slipping-force test as per IS 8710-1978

D.C. Power Supply UnitMag/Demag UnitOperating Pendant

Designed for Safe & Reliable Operation

The Circular Electromagnetic Chuck is designed for grinding operations and operates on a continuous D.C. power supply. The control system incorporates supply protection and clear magnet ON and demagnetizing-cycle indications for dependable operation.

Rotary Magnetic Face

The coil is stationary and the middle magnetic face rotates with the machine spindle.

Inspection & Safety Checks

  1. Check the resistance to the earth terminal.
  2. Perform the de-magnetizing test to verify proper demagnetizing operation.
  3. Carry out the high-voltage test for electrical insulation.
  4. Perform the leak-proof test to verify the chuck's electrical integrity.
  5. Conduct the sleeping-force test as per IS: 8710-1978.
  6. Use the specified 230 V A.C. input supply and 110 V D.C. operating output.
  7. Ensure the A.C. and D.C. supply circuits are protected using the specified fuses and MCB.

Operation Sequence (Follow the steps)

01

Mount and align the chuck on the cylindrical grinding machine spindle.

02

Connect the stationary coil to the D.C. power-supply or Mag/Demag unit.

03

Clean the rotary magnetic face and workpiece contact surface.

04

Position the ferrous workpiece correctly on the magnetic face.

05

Switch Magnet ON and confirm rigid holding before spindle rotation.

06

Perform cylindrical grinding while the face rotates and coil remains stationary.

07

Stop spindle rotation and initiate the demagnetizing cycle.

08

Remove the workpiece only after demagnetization is complete.

Available Sizes

Available chuck dimensions are specified by diameter × height.

Model Code Size (Dia. × H)
002-06-01 Dia. 100 × 100 mm
002-06-02 Dia. 150 × 150 mm
002-06-03 Dia. 200 × 200 mm

Applications

Mag Demag unit with pendant for cylindrical grinding chuck
Mag/Demag Unit with Pendant

A D.C. power-supply unit or Mag/Demag unit is required for operating the cylindrical-grinding chuck.

Need help choosing a model?

Share your load details with our team.

WhatsApp
Call Us